On this page
Liquid and sauce configurations to compare

Lotion and cream sachet packer
A piston-dosed sachet configuration for cosmetic lotions and creams.
- Piston pump dosing
- Film forming and sealing
- Contact materials selected for the formulation

Wasabi and mustard stick packer
A stick-pack configuration for viscous condiments, with piston dosing.
- Back-sealed sticks
- Product hopper above the lanes
- Tooling selected for the finished pack

Hand sanitizer sachet packer
A liquid or gel sachet configuration; include the formulation in your enquiry.
- Four-side seal format
- Piston pump dosing
- Alcohol content: review required

Ketchup sachet packer
Roll-film forming, piston dosing and four-side sealing for tomato sauces.
- Rotary-valve piston pump
- Printed-film registration
- Application-specific dose and lane layout
Start with the closest product and pack format. The quotation defines the actual dosing equipment, lane layout and options for your material.
Download the liquid and sauce configuration brief (PDF) to share the project inputs with your team.
Choose a stick pack or a flat sachet
These machines form portion packs from roll film. A back-sealed stick suits a narrow pack; a flat sachet uses a three-side or four-side seal layout. Confirm the finished drawing and opening style before selecting tooling.
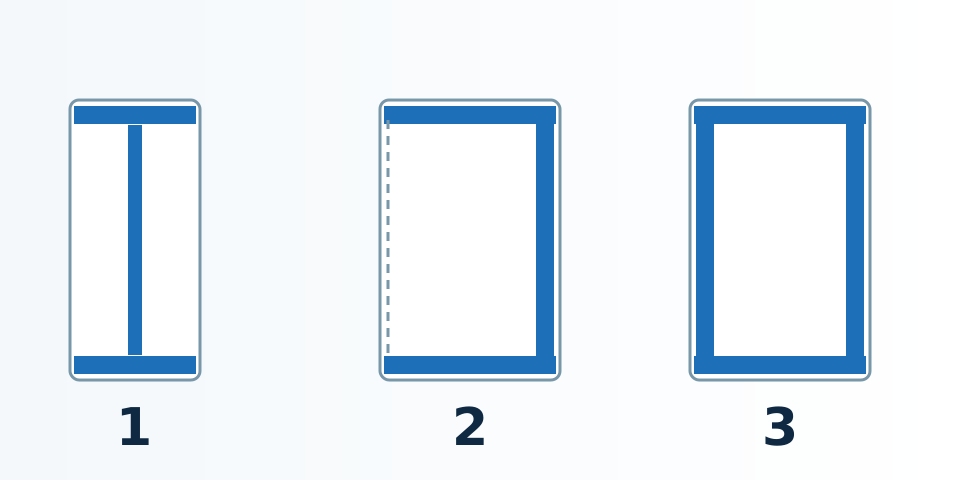
- 1. Back-sealed stick
- 2. Three-side seal sachet
- 3. Four-side seal sachet
Compare the stick pack family and sachet packing family for the format overview. For a pouch already made by a converter, use premade pouch filling; for foil-sealed cups or honey cap cavities, use filling machines.
Keep sauce out of the seal
The ketchup reference uses a rotary-valve piston pump to meter the dose while the machine forms, fills, seals and cuts the film. For viscous sauce, the nozzle cut-off and product temperature need the same attention as the pack format.
Our anti-drip ketchup configuration and energy gel stick configuration incorporate pneumatic shut-off/suck-back nozzles and heated jacketed hoppers with agitators. Suck-back draws residual product away from the nozzle tip while the jacketed hopper maintains target viscosity before dosing.
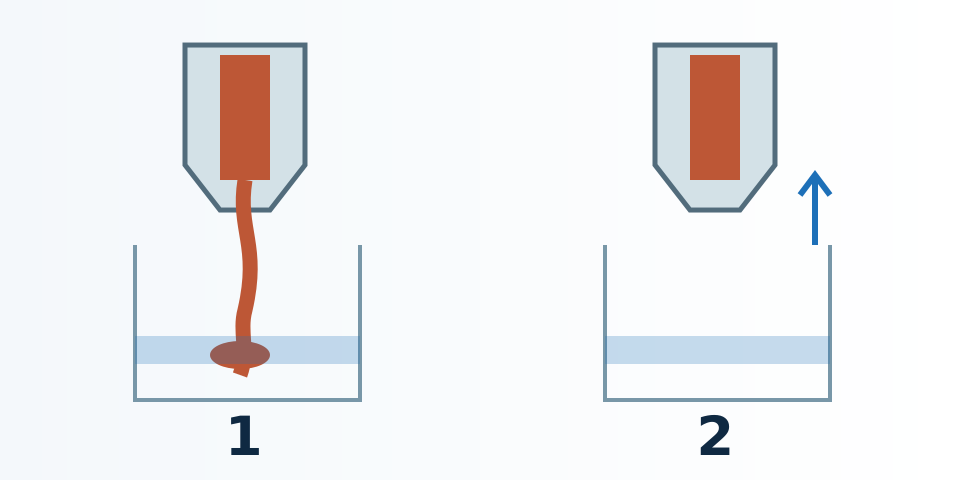
- 1. Product tail reaches the seal band
- 2. Cut-off and draw-back keep the band clear
| Product behavior | Dominant failure mode | Prevention to confirm |
|---|---|---|
| Stringing or dripping | Product enters the closing seal | Nozzle cut-off/suck-back and dosing timing, verified with your liquid |
| Temperature-sensitive flow | Flow and dose vary as the product cools | Jacketed hopper and agitation where needed; product temperature specified for your process |
| Particles or seeds | Nozzle blockage or uneven solids distribution | Particle-oriented mustard configuration; confirm passage and mixing |
| Foaming | Foam carries liquid toward the seal | Shampoo anti-foaming dosing; confirm on the formulation |
If a product tail still reaches the seal area, resolve nozzle behavior and timing in the trial before accepting the output target. There is no universal viscosity cut-off or suck-back setting for all sauces.
Parameters to confirm in the quotation
Each multi-lane liquid and sauce build is sized around your dose volume, finished pack width and product viscosity. The table below summarizes our standard engineering configuration ranges and what fixes each parameter.
| Parameter | Standard configuration range | What fixes it |
|---|---|---|
| Dose and fill tolerance | 1–50 ml (piston cylinder sized to target dose) | Target in ml or g, product density and agreed trial measurements |
| Lane count and output | 2–16 lanes at 20–50 cuts/min | Pack drawing, film width and accepted packs per hour |
| Nozzle and hopper | Rotary-valve piston pump with pneumatic shut-off / suck-back nozzle | Viscosity at fill temperature, stringing, foam and particles |
| Contact parts and cleaning | SUS304 or SUS316L contact parts; jacketed agitated hopper for warm sauces | Formulation, cleaning method and product changeovers |
| Utilities and footprint | 220 V / 380 V, 50/60 Hz; 0.6–0.8 MPa compressed air | Site voltage, phase, frequency, air supply and line layout |
Agree the sample trial before shipping material
Use representative product and production-specification film at the intended filling temperature. Agree the quantity, delivery address, any trial cost and return samples with LINEVO before shipping.
| Trial item | Record and agree |
|---|---|
| Fill | Target and tolerance; weighed samples from every running lane |
| Drips and seals | Nozzle tail clearance and clean seal zones; agreed strength and leak checks |
| Good output | Cut rate, lanes, timed run, rejects and stoppages |
| Changeover | Contact parts removed, cleaning steps and material used on restart |
ASTM F88/F88M-23 measures the force required to separate a sealed test strip and identifies its failure mode. Pair tensile seal-strength tests with burst/squeeze leak checks at your target fill weight and temperature. See sample-test preparation.
Compare good output and running costs
Compare accepted packs over the same production period. Cuts per minute need the running lane count, downtime and reject rate before they describe usable output.
Accepted packs/hour = running lanes × cuts/min × 60 × running fraction × acceptance rate. On an 8-lane machine running at 30 cuts/min with 80% net running time and 98% acceptance, hourly output is 11,290 accepted packs/hour.
Ask each quotation to identify film and product lost during startup, cleaning labor, format-change parts and wear spares. Price downstream counting or cartoning separately when needed, and include a spare-parts plan. This exposes costs that the purchase price alone leaves open.
Send your liquid and pack brief
Send the product name, fill target, pack drawing or sample, film specification and required good output. Include viscosity with its measurement method and temperature, plus any particles, foam or stringing. Mark unknown values for review.
Use WhatsApp or the project brief checklist to request a configuration review and agree the sample trial.
Sources
Updated October 21, 2026. Our liquid configurations combine rotary-valve piston dosing, nozzle shut-off and multi-lane film sealing around your product. The ketchup sachet configuration and energy-gel stick configuration incorporate suck-back nozzles and jacketed hoppers with agitation, summarized in the liquid and sauce specification sheet.
Standards reference: ASTM F88/F88M-23, Standard Test Method for Seal Strength of Flexible Barrier Materials, used to verify seal integrity during sample testing.
Guides for this application
What to send us
Send what you have and mark what is still undecided. Discuss your application with LINEVO.
| Item | Why we need it | Example format |
|---|---|---|
| Product and behavior | Selects dosing and nozzle requirements | Product name; viscosity with method and temperature; particles, foam or stringing |
| Dose and pack | Defines format tooling and fill review | Fill in ml or g; density for mass targets; finished drawing or sample |
| Film and output | Defines sealing and lane layout | Film structure and roll width; good packs/hour; shifts and changeovers |
| Trial and site | Defines acceptance and quotation scope | Product/film sample availability; cleaning needs; power and air supply |