On this page
Packaging line design in seven steps
Work through the steps in this order. Each one uses the result of the one before, and each has its own section below.
- Products and formats: every product and pack size the line must run, and the good output each one needs per shift
- Process map: each step from feeding to the pallet, with the units you already have
- Primary packaging route: chosen from the finished pack; the packaging machine families by process cover this step
- Line rate and balance: which unit sets the rate, with every unit converted to the same count
- Layout: straight, L-shaped or U-shaped, from the room and the material flow
- Interfaces and responsibilities: transfers, signals, utilities and who supplies each unit
- Acceptance: what a run of the combined line must show before handover
Map the process from feeding to discharge
Primary packaging puts the product into the pack that touches it: a bag, stick, sachet, pouch, cup or bottle. Secondary packaging groups those packs into cartons, overwrapped boxes or cases, and the end of the line closes the cases and builds the pallet.
Record how product reaches the packaging machine, how the dose is prepared and how completed packs leave the machine. Add coding, inspection, grouping or secondary packaging where the project requires them.
- Product feeding and buffering
- Dosing and primary packaging
- Coding and inspection requirements
- Discharge and downstream handling
- Secondary packaging such as cartoning, overwrapping or case packing
- Case sealing and palletizing
Typical combinations
Our engineering team combines the equipment families around the process you need. The proposal names each unit, the existing equipment it connects to, and the mechanical and control interfaces between them.
- Powder bagging: product feeder, auger filler, VFFS machine and discharge conveyor, with dust extraction where needed
- Weighed solids: product elevator, multihead weigher on a support frame, VFFS machine, output conveyor, then optional checkweighing and metal detection
- Single-serve to retail box: stick pack or sachet machine, counting, cartoner with leaflet insertion and coding, then optional overwrapping
- Multi-lane sticks or sachets to the pallet: multi-lane machine, counting discharge conveyor, bagging or cartoning, weight checking, case packing, case sealing and robotic palletizing; the counting conveyor takes the place of a separate bag-sorting machine
- Premade pouches: pouch magazine, pouch filler with weigher, auger or pump, then coding and discharge
- Pouches into wrapped retail boxes: pouch packer, weighing scale, cartoner and cellophane wrapper in a straight or corner run, as in our hookah and shisha packaging lines
- Trayed or grouped products: infeed conveyor, flow wrapper, coding and, where required, cartoning
- Containers: filling and capping, then labeling, with coding and inspection as needed
Balance the line around its slowest step
A line produces at the rate of the unit that runs slowest or stops most often under your conditions, not at the rate of its fastest machine. Dosing time for a sticky product, seal time for a thick laminate and carton loading for an irregular product are typical limits.
Compare each unit on the same product, pack and format, and allow buffer space or accumulation between units so that a short stop in one place does not immediately stop the whole line.
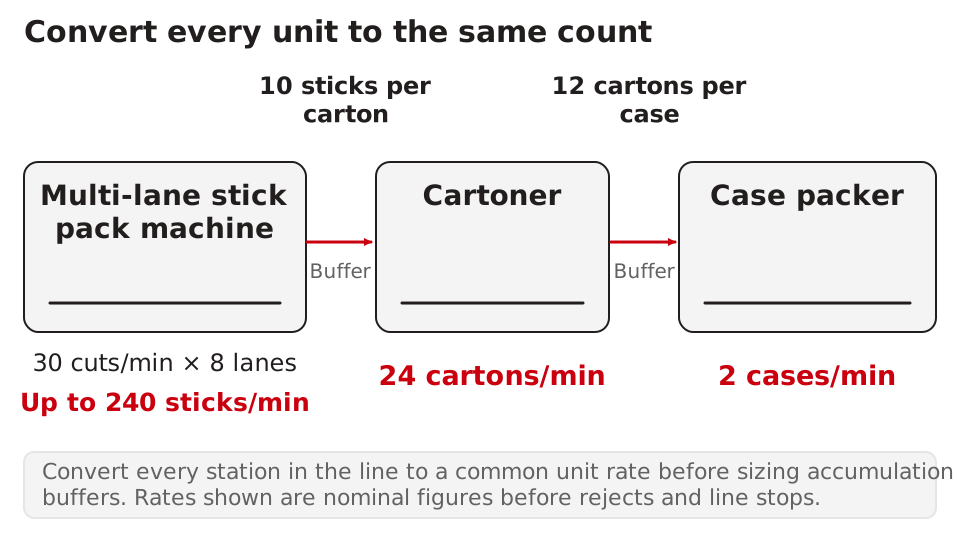
Convert every unit to the same count before comparing them. A multi-lane stick pack machine is listed in cuts per minute, a cartoner in cartons per minute and a case packer in cases per minute. For example, 30 cuts per minute on 8 lanes forms 240 sticks per minute; packed 10 to a carton, the cartoner must run at 24 cartons per minute, and at 12 cartons to a case the case packer needs 2 cases per minute before rejects and stops. Confirm the exact lane count and cycle speed on your product and film during the application review.
A common design choice is to let the units after the rate-setting one run somewhat faster, so that they can clear the buffer after a short stop. The margin, the buffer length and the stop signals are agreed for each project.
To improve an existing line, record where it stops and for how long over several shifts. The unit with the most stop time or the lowest good output is where a change usually pays off first, whether that is a dosing adjustment, a longer buffer or a faster downstream unit.
Choose a layout: straight, L-shaped or U-shaped
The layout follows the room and the flow of product and materials. These are the common shapes and what each one asks of the site:
- Straight (in-line): units in one row, with product entering at one end and leaving at the other. Transfers are simple and each unit can be reached from both sides, but the line needs a long room and puts the product supply and the finished goods at opposite ends.
- L-shaped: the line turns through 90 degrees, usually on a conveyor between two units. It fits a shorter room or a corner; check how the product turns and whether its orientation must be kept through the corner.
- U-shaped: the line returns alongside itself, so the infeed and the outfeed are on the same side and one team can watch both ends. It is compact, but leaves less room between the two legs, so plan access for maintenance and for loading film, cartons and labels.
- Several machines into one: two or more primary packaging machines feed one cartoner or case packer when that unit can take the output of more than one machine. The merge point needs its own buffer and control signals.
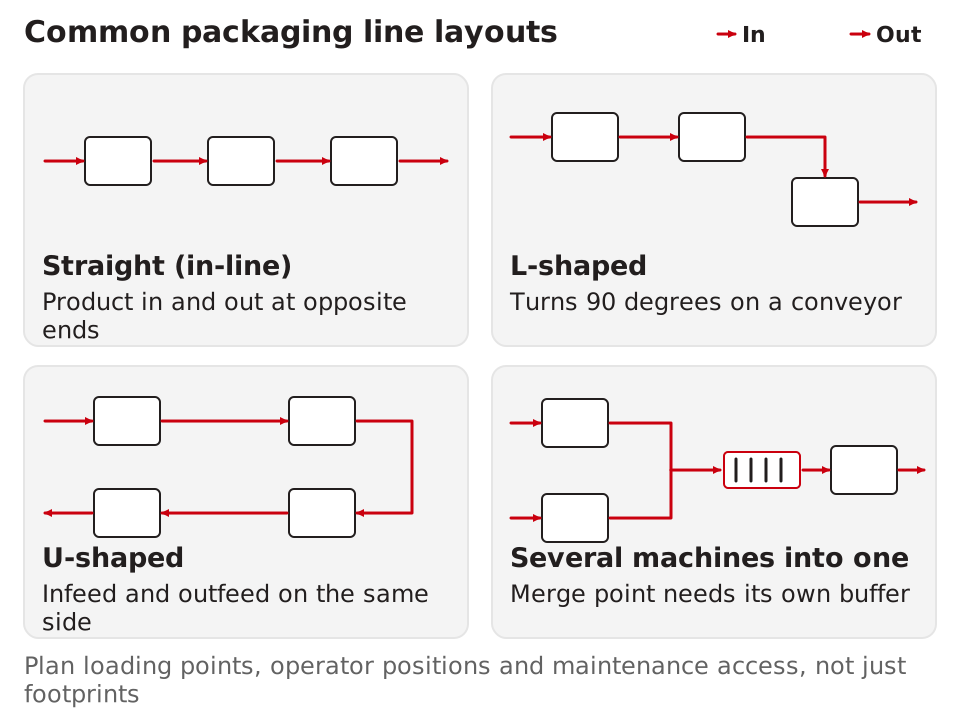
Draw the layout with the loading points for film, cartons and labels, the operator positions and the maintenance access, not just the machine footprints. The installation and training preparation page lists the site details to collect with it.
Make integration boundaries explicit
We coordinate the mechanical transfers, controls and utilities for the proposed system. Our layout review identifies the units supplied by each party and the system-level checks needed for acceptance.
- Transfer heights, directions and product orientation between units
- Signals exchanged between machines, such as run, stop, full, empty and reject
- Power, compressed air and any vacuum or nitrogen supply for each unit
- Platforms, conveyors, guarding and operator access
- Existing equipment on site that the new units must connect to
Plan formats and changeovers
List every product and pack size the line must run and how often it changes. A new bag width, stick width, pouch size, carton size or container shape can require its own change parts or settings on more than one unit. Agree which formats are included in the quotation and how changeovers are documented.
Before you automate: limits and preconditions
Automatic packing is not the right next step for every product or volume. Its limits are worth stating before any machine is chosen:
- Flexibility: each new pack size, film or carton can need change parts and settings on more than one unit, so many short runs of different formats spend a large share of the shift in changeover.
- Consistent inputs: a machine sets its dose, seal and cut for a product and material within a range. Product that changes in flow or density, or film and cartons that vary between deliveries, show up as rejects and stops.
- Coupled stops: in a line, a stop in one unit stops its neighbors as soon as the buffer between them is full or empty.
- Skills and parts: operators need training for setup, changeovers and cleaning, maintenance staff for adjustments and wear parts, and spare and change parts need to be on hand.
- Site and integration work: plan floor space, power, compressed air and the connections between units as part of the line proposal.
Automation is most likely to pay off when the product and pack are settled, the volume keeps the machine running for most of the shift, the materials are consistent and there are people to run and maintain it. If one of these is not yet true, a sample test or a single machine is often the better first step.
One machine first, or the whole line?
Start with one machine when one manual step limits output or takes the most labor, often dosing and primary packaging, when volumes are still growing, or when the product's behavior on a machine is still uncertain. Specify that machine with the next step in mind: the discharge height and direction, the signals it will exchange and the space for the unit that follows.
Plan the whole line at once when the products, formats and volume are known, when a new room or plant is being laid out, or when the units must be matched from the start, for example when sticks are counted straight into cartons.
To add units in stages, keep a written record of the interfaces fixed for the first machine, so that the next quotation works to the same transfer and signal definitions.
What to specify when buying a complete line
Two complete-line quotations can only be compared when they state the same scope. Ask each supplier to state:
- Every unit in the scope with its model or configuration, and the units that are excluded or supplied by others
- The products and formats included, with the change parts for each
- The line output in good packs, cartons or cases per minute, the product, format and run length it refers to, and the unit that sets it
- The buffers, conveyors, platforms and guarding between units
- The signals that pass between units and who programs them
- The utilities for the whole line: power at each position, compressed air and any nitrogen or vacuum
- Who coordinates installation, commissioning and the acceptance run of the combined line
- The training, documents, and spare and change parts included
If the units come from several suppliers, name one party responsible for integrating them and for the acceptance of the combined process; otherwise the gaps between the quotations become yours to close. The project brief checklist collects the product, format and site details such a request needs.
Agree on a system-level check
A component specification does not by itself describe the output of a complete line. Define the material, formats, operating conditions and acceptance measurements for the proposed combination.
Useful measurements include fill weight or volume across a sample of packs, seal and pack appearance checks, the count of good packs over a timed run, and the number and causes of stoppages. Record the product batch and packaging materials used so the result can be compared later.
Discuss a system
Send a simple sketch of the process, the products and formats, the units you already have, the units you need and the output you are aiming for. Our engineering team reviews how the packaging machine and the surrounding equipment could be combined and where a sample test would settle an open question, and comes back with a proposal to discuss.
What to send us
Send what you have and mark what is still undecided. Discuss your application with LINEVO.
| Item | Why we need it | Example format |
|---|---|---|
| Product and its behavior | Powder, granule, liquid, paste or solid pieces decide the dosing method and the parts that touch the product. | Free-flowing granules, with a photo of the product |
| Finished pack and fill | The pack style, its size and the fill per pack set the format and the dosing range. | Pillow bag, 100 × 150 mm, 50 g per bag |
| Target output | Output per minute or per shift decides the number of lanes and the model size. | 60 good packs per minute, one shift per day |
| Packaging material | Film or container type affects sealing, forming and the settings we confirm. | Laminated roll film, 250 mm wide, or the film datasheet |
| Site and destination | Power supply, compressed air and destination country decide the electrical and utility scope. | 380 V, 3-phase, 50 Hz, delivery to Germany |